About 100Kg Per Feet Crate Conveyor System
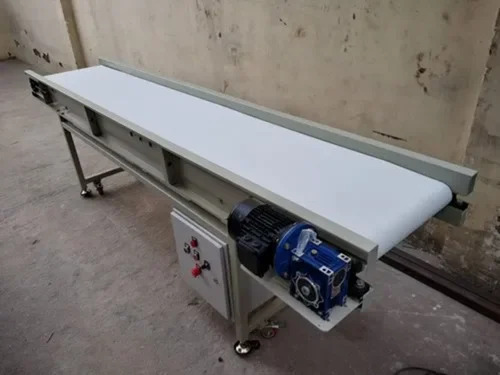
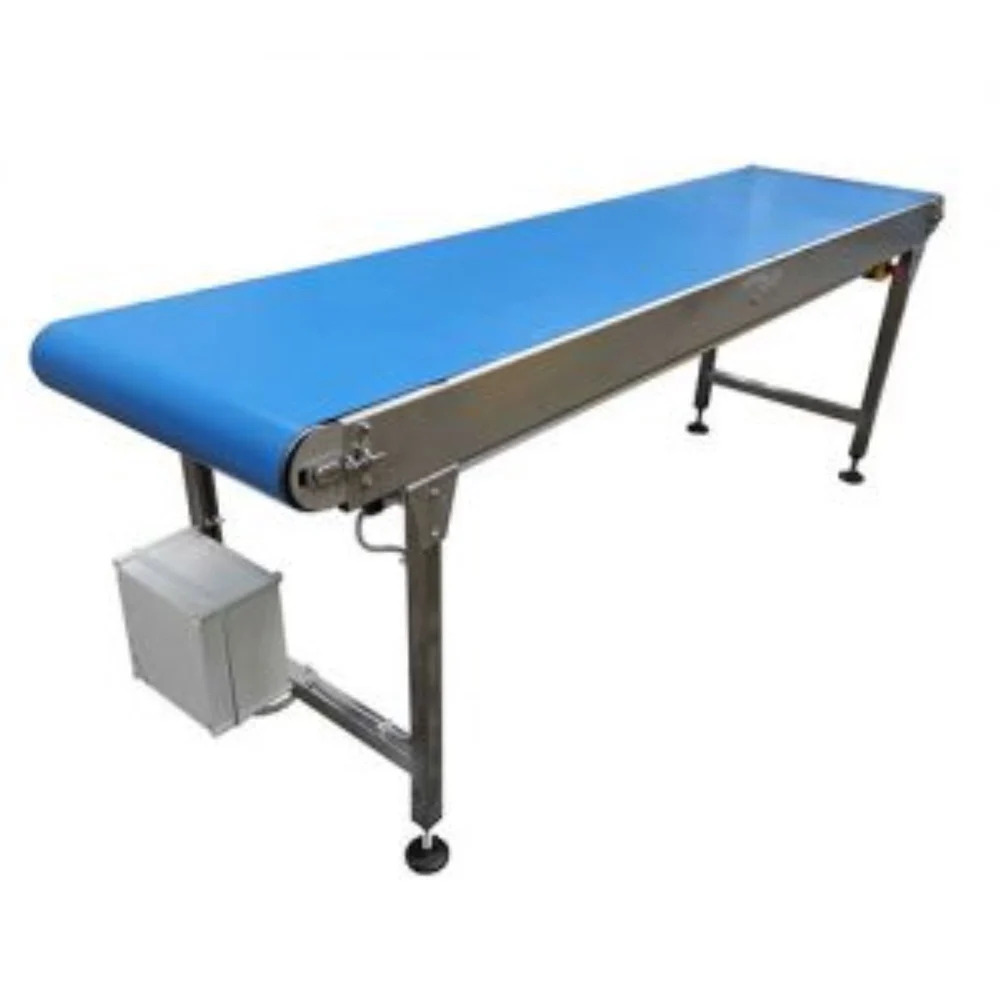
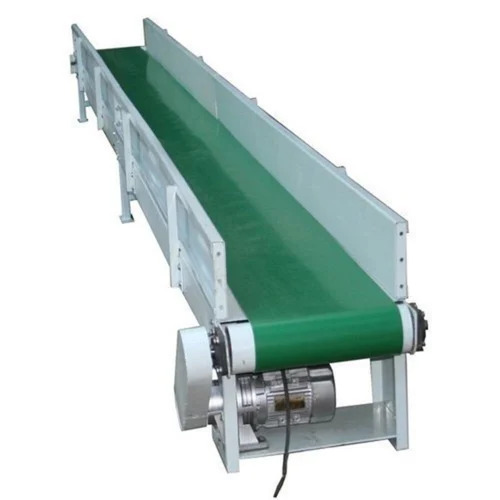
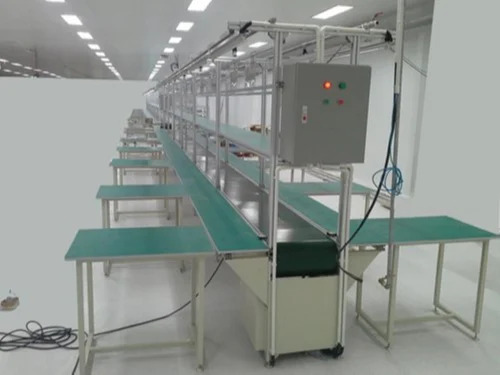
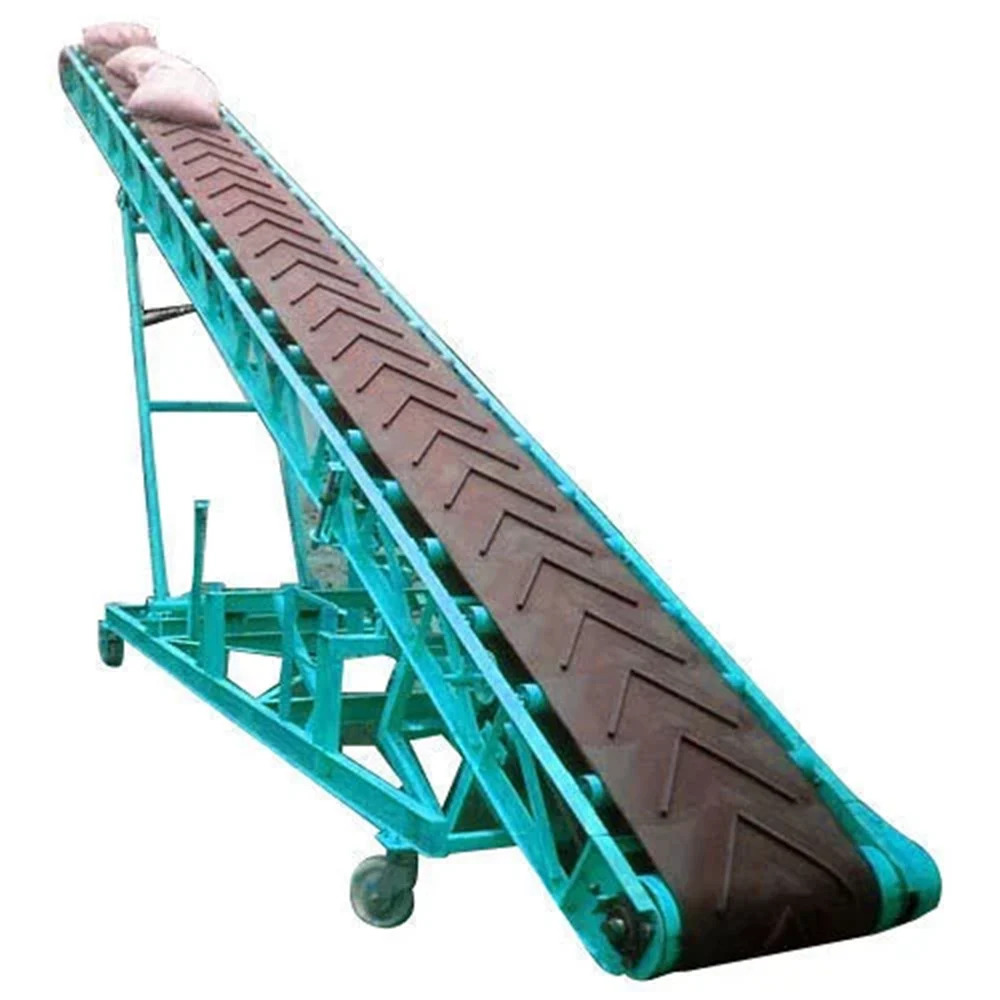
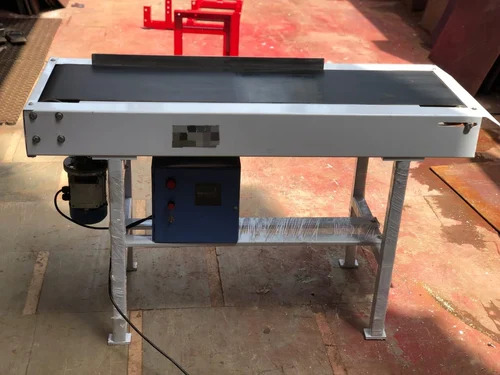
Find sensational efficiency with our 100Kg Per Feet Crate Conveyor System, masterful for bottling and crate handling operations. Its sizzling flat PVC belt and powder-coated mild steel structure ensure stellar durability and corrosion resistance. Designed with a straight system layout and variable speed, this conveyor delivers continuous duty for high-demand environments. With automatic controls, an included diverter, and height adjustability, shop now for seamless integration in your facility. The low-noise, easy-maintenance design, emergency stop button, and geared motor drive promise safe and reliable performance every time.
Commercial Uses and Direction of Use
This 100Kg Per Feet Crate Conveyor System is ideal for commercial bottling facilities and crate handling operations, offering versatile usage across numerous industries. Its straight layout and automated controls support efficient crate movement, while the diverter enables smart distribution. Simply position the crates on the belt at the start point-height adjustable for ergonomic use-and let continuous, geared motor-driven power transport loads swiftly. Designed for installation on floor surfaces, it ensures safe, streamlined processing in any industrial setting.
Supply Ability, Sample Policy & Export Markets
With robust supply capacity, we can handover sizable quantities of 100Kg Per Feet Crate Conveyor Systems to meet urgent demands. Sample evaluations are available on request, allowing you to assess quality before finalizing the list price. We serve a wide range of export markets, including but not limited to Asia, the Middle East, and Africa. Our tailored solutions and reliable global logistics ensure timely delivery-whether for manufacturers, suppliers, or traders across India and beyond.
FAQ's of 100Kg Per Feet Crate Conveyor System:
Q: How does the 100Kg Per Feet Crate Conveyor System enhance bottling operations?
A: The conveyor streamlines crate handling in bottling setups by providing automatic, continuous-duty movement, reducing manual labor while boosting efficiency and safety.
Q: What is the recommended maintenance process for this system?
A: Maintenance is straightforward-regularly inspect the belt and geared motor, clean the powder-coated surfaces, and check the emergency stop button functionality for optimal performance.
Q: Where can the system be installed for best results?
A: It is designed for floor-mounted installation in commercial or industrial environments, such as bottling plants and warehouses, ensuring stable and secure operation.
Q: When should the diverter accessory be used?
A: The diverter is advantageous when sorting or directing crates to different bottling lines, helping manage workflow and increase operational flexibility.
Q: What are the primary benefits of the geared motor drive and automatic features?
A: The geared motor ensures powerful, reliable movement even under heavy loads, while automatic operation and adjustable speed deliver precise control and reduced downtime.



 Send Inquiry

 Send Inquiry


